
Packaging Film Coefficient of Friction (COF): Testing and Targets
Packaging film coefficient of friction explained: static vs kinetic COF, ASTM D1894 testing, slip additive migration and how to set COF targets for your machine.
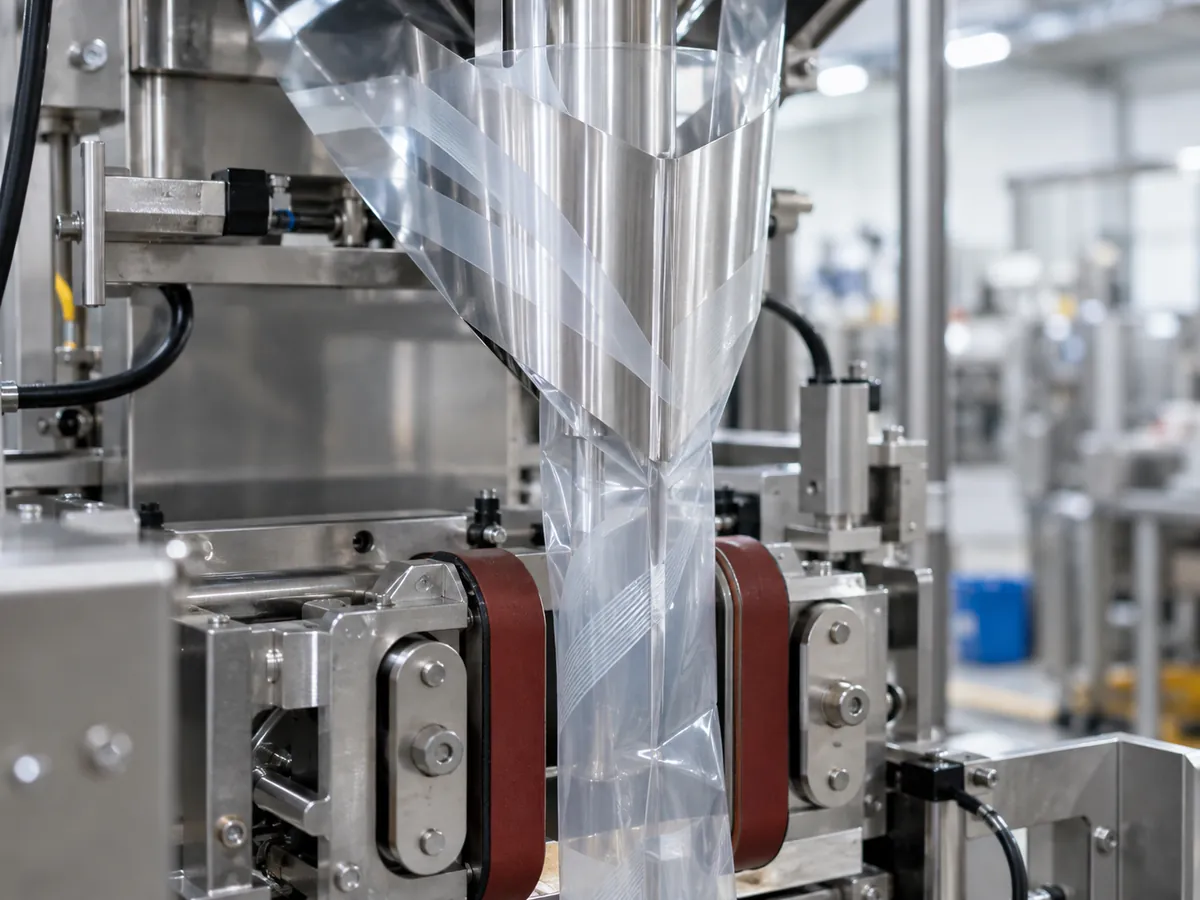
Excess friction can drag film over a collar; insufficient grip can let pull belts slip. Packaging film coefficient of friction (COF) is a dimensionless number that describes how easily one surface slides over another. For film, it is measured as the ratio of the force needed to slide a weighted sled to the weight of that sled. A low COF means the film slides easily and a high COF means it grips. Both extremes cause trouble on a packaging line, so COF appears on almost every film data sheet.
COF quick check
Scroll horizontally to view all columns if needed. ↔
| Input | Record | Why it matters |
|---|---|---|
| Static / kinetic | Both dimensionless values | Starting motion and running motion differ |
| Surface pair | Film/film or film/metal, named sides and finish | A result belongs to the tested pair |
| Film age | Time since extrusion/conversion and storage history | Migratory slip can change the surface |
| Test setup | Sled, speed, temperature and RH | Conditions affect comparison |
What film COF measures
Film COF compares two surfaces: film against film, or film against another material, usually polished metal. The value depends on the pair, not on the film alone. A film can have a low COF against itself and a high COF against stainless steel, or the reverse, because slip additives, surface treatment, roughness and antiblock particles affect each pairing differently.
COF is a surface property. It says nothing about seal strength or barrier, but it strongly affects how a film behaves on forming shoulders, pull belts, conveyors and in stacked cartons. The other film properties are covered under packaging film performance.
Static vs kinetic COF
Every COF test reports two numbers.
- Static COF is the force needed to start the sled moving, divided by the sled’s normal load, so it has no units. It reflects how much a stationary film sticks to a surface. It matters when a film starts from rest: a stack of packs about to slide, a web restarting after a stop, or a bag held against a belt.
- Kinetic COF is the force needed to keep the sled moving at steady speed, again divided by the normal load. It is usually the lower of the two, and it governs film that is already running over a collar or a roller.
The gap between them matters as much as either value. A large difference can cause stick-slip behavior, where the film jerks instead of gliding. On a vertical machine that appears as uneven bag length or chatter at the forming collar.
COF test method: ASTM D1894 in principle
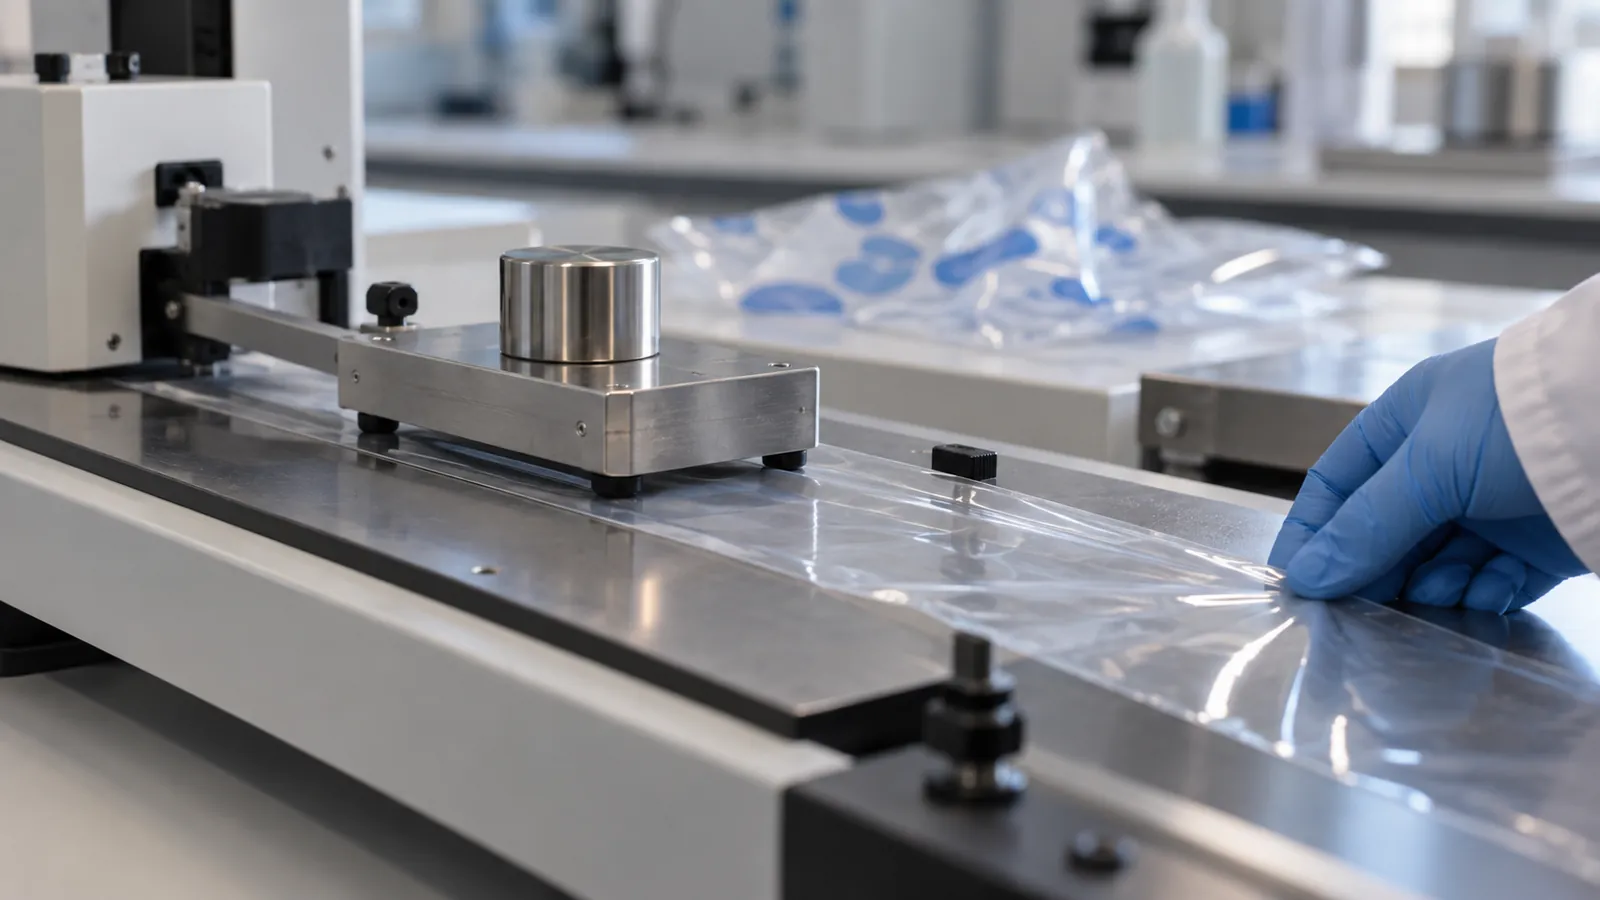
ASTM D1894-24 is the standard for static and kinetic COF of plastic film and sheeting. In principle, a sled of defined weight wrapped with one film sample is pulled across a second film sample (or a metal plate) clamped on a flat bed at a defined speed. A load cell records the pull force. The initial peak gives the static value, and the average force during steady sliding gives the kinetic value.
Results depend on the details, so write them into the specification:
- Surface pair: inside to inside, outside to outside, inside to outside, or film to metal.
- Sled weight and contact area, and the speed of pull.
- Conditioning: temperature, humidity and how long the film was aged before the test.
- Which side of the web faces which surface, and the direction of the pull relative to the web.
Two data sheets that quote COF are only comparable if these match. Ask the supplier for the full method as well as the number.
Film-to-film vs film-to-metal
Film-to-film COF describes sliding against itself. Blocking is adhesion between adjacent layers, so difficult unwinding needs a separate blocking check as well as COF. Film-to-film COF affects how packs slide against each other in a case, and how a formed tube moves past the film layers above it. Film-to-metal COF describes how the web passes over stainless steel parts such as forming collars, sealing jaw covers and guide bars. On VFFS machines, the metal value is often the more critical one because the film is pulled across the collar under tension.
Many films are made with different surfaces on each side, for example a printed outer layer and a heat-seal inner layer, so the COF is specified separately for each. A film-to-film test of the sealant against the sealant says little about how the printed side slides on a belt.
Slip additives, migration and bloom
Polyethylene and polypropylene sealants often contain slip additives such as erucamide or oleamide. These are fatty acid amides dissolved in the polymer while it is hot. After the film cools, they migrate slowly to the surface and form a thin lubricating layer. This is called bloom.
This has practical consequences:
- Time. Freshly extruded film may have a higher COF than the same film a few days later, because the additive has not yet reached the surface. A film can run differently on the day it arrives than after weeks in the warehouse.
- Temperature. Storage and test temperature can change the slip response. Do not assume every warm-stored film has lower COF; compare samples at recorded ages and temperatures for the actual additive system.
- Transfer. Slip can transfer from one layer to the other when a roll is wound, so the outer surface of a laminate can pick up additive from the inside. In a laminated structure, additive can also migrate into the adhesive or interfere with the bond or seal if the level is high.
- Seals and print. Excess surface additive can weaken seals, hurt adhesion of coatings or inks, and leave residues on machine parts.
So specify COF at the point of use and, where possible, at the end of the expected storage time as well as at delivery. Slip systems are most common in polyethylene film and BOPP film.
How COF affects the packaging line
Scroll horizontally to view all columns if needed. ↔
| Area | Effect of COF too high | Effect of COF too low |
|---|---|---|
| Forming collar | Drag, higher tension, wrinkles, wandering tube | Little problem at the collar, but may signal poor tension control |
| Pull-down belts | Usually grips well | Film slips on belts, bag length varies, registration drifts |
| Roll unwind | Sliding drag; assess layer adhesion (blocking) separately | Low sliding resistance may complicate winding; check tension too |
| Stacking and case packing | Packs resist sliding, harder to align and load | Packs slide in cases and on pallets, cartons shift |
| Conveyors and chutes | Packs hang up or tip | Packs slide off or crowd unpredictably |
| Seal area | Rarely an issue | Excess surface slip can reduce seal strength |
The same film can sit in the right range for one machine and the wrong one for another. A film that slides well over a collar may be too slippery for a high-speed flow wrapper with narrow belts, and a high-grip film may be acceptable on a slow machine with lightly loaded jaws. For a horizontal machine, the equivalent page is flow wrap film.
Why COF targets differ by machine
There is no universal COF number. The right target depends on the machine design, the pull-down method (belts or rollers), the collar material and finish, the film tension, bag size, speed and the product. Qualitatively:
- Low COF suits machines where the film must glide over long metal contact paths, or where packs must slide into cartons.
- Medium COF is the usual compromise for general-purpose film on belt-driven vertical machines, since belts need grip and collars need glide.
- High COF suits cases where packs or sacks must stay put on pallets, or where the machine relies on friction drive.
Do not copy a number from another line. Ask the machine supplier for the COF range they recommend for film-to-metal and film-to-film, and write that range into the film specification along with the test method. The VFFS film page shows how this fits with other machine requirements.
Common COF problems
Scroll horizontally to view all columns if needed. ↔
| Problem | Likely cause | What to check |
|---|---|---|
| Film drags at collar, wrinkles | Metal COF too high, worn or scratched collar, high tension | Film-to-metal kinetic COF, collar finish, tension setting |
| Bag length varies, belts slip | Film too slippery, dirty belts | Outside-surface COF, slip additive on belts, belt wear |
| COF changes over storage | Possible slip migration or changed conditions | Repeat paired tests at recorded temperature and film age |
| Run differs between lots | Additive level or aging differs | Lot COF data and age at test |
| Weak seals after slip bloom | Surface additive in seal area | Seal strength against COF, additive level |
| Packs slide in case or on pallet | Outer surface too slippery | Film-to-film COF of the outside, anti-slip coating |
| Static COF much higher than kinetic | Stick-slip | Both values, antiblock level, surface treatment |
COF test and symptom record
Copy this blank record for each lot and each surface pair; agree limits from a line trial rather than a universal target.
Scroll horizontally to view all columns if needed. ↔
| Field | Entry |
|---|---|
| Lot, structure, extrusion/conversion date | _____ |
| Pair, inside/outside faces, MD/TD pull, metal finish | _____ |
| D1894 edition, sled mass/contact area, pull speed | _____ |
| Conditioning time, test temperature / RH | _____ |
| Film age at test, storage temperatures | _____ |
| Static / kinetic result and agreed range | _____ |
| Machine, speed, tension, collar or belt symptom | _____ |
| Separate blocking result if unwind layers adhere | _____ |
| Corrective change and repeat-trial result | _____ |
Use the symptom table to select a check, then record the result here. Compare the actual collar and belt contacts before changing slip dosage. Comparing film specifications helps align supplier reports.
Frequently asked question
What is the coefficient of friction for polypropylene?
There is no single value for a polypropylene film. The result belongs to a tested grade, surface pair, age and conditioning history. Ask for both static and kinetic values on the surfaces your line contacts, using the agreed D1894 setup.
Sources and method
Reviewed October 8, 2026. D1894-24 covers starting/sliding friction on defined surface pairs. A manufacturer’s public slip-additive note describes time-dependent bloom; its slip-system overview distinguishes migratory and non-migratory systems and temperature performance. A public antiblock note distinguishes adhesion from sliding. These are supplier explanations, not site measurements or product recommendations; no dosage or COF target is adopted here.
Continue reading
Related articles
Hot Tack in Packaging Films: What It Is and Why It Matters
Hot tack packaging performance is the strength of a heat seal while it is still molten. Learn the ASTM F1921 test, the hot tack curve and how it affects VFFS lines.
Oxygen Transmission Rate (OTR): Units, Test Methods and How to Read It
Oxygen transmission rate (OTR) measures how much oxygen passes through a film. Learn the units, test methods, conditions and how OTR relates to shelf life.
Packaging and Shelf Life: How Film Choice Affects It
Packaging film shelf life depends on oxygen, moisture, light and seal integrity. Learn the failure modes, real-time vs accelerated tests and a study checklist.