
Premade Pouch Packaging Materials: What Pouch Machines Need
Premade pouch packaging materials explained: tolerances, stiffness, sealants, zippers and the specs pouch machines need to open, fill and seal reliably.
Failed pickup, opening or top sealing stops the line and can waste filled product. Check the actual pouch drawing against the machine’s grippers, opening station and final seal band before approving material.
Scroll horizontally to view all columns if needed. ↔
| Checkpoint | Drawing / trial input | Record the loss |
|---|---|---|
| Gripping | Width, height, squareness and corner grip zones | Missed picks / crooked pouches: ___ |
| Opening | Panel behavior, mouth clearance and zipper opener | Failed opens / stoppage minutes: ___ |
| Static | Double picks and panel adhesion under trial conditions | Double feeds / rejected pouches: ___ |
| Top seal | Final seal-band location, jaw access and contamination | Filled rejects / leak results: ___ |
How premade pouch machines handle pouches
The machine sequence explains most pouch specifications.
- Magazine or feeding: pouches are stacked in a magazine or fed from a conveyor. Stack height, shingling and how the pouches sit determine whether a single pouch is picked reliably.
- Gripper pickup: suction cups or mechanical grippers take the front panel and transfer the pouch to a pair of grippers that hold the pouch by its top edge corners.
- Opening: suction cups pull the front and back panels apart, often assisted by a puff of air. For zippered pouches, a zipper opening station may press or pull the zipper open.
- Filling: product drops or is dosed into the open mouth. The pouch has to stay open and hang square.
- Sealing: heated jaws seal the top, sometimes in two passes, followed by cooling bars and sometimes embossing. For a top-filled zipper pouch, locate the final seal band from its drawing; do not assume it crosses the zipper profile.
Grippers handle the pouch and pull it open many times a minute, so small differences in shape, stiffness or static have a big effect.
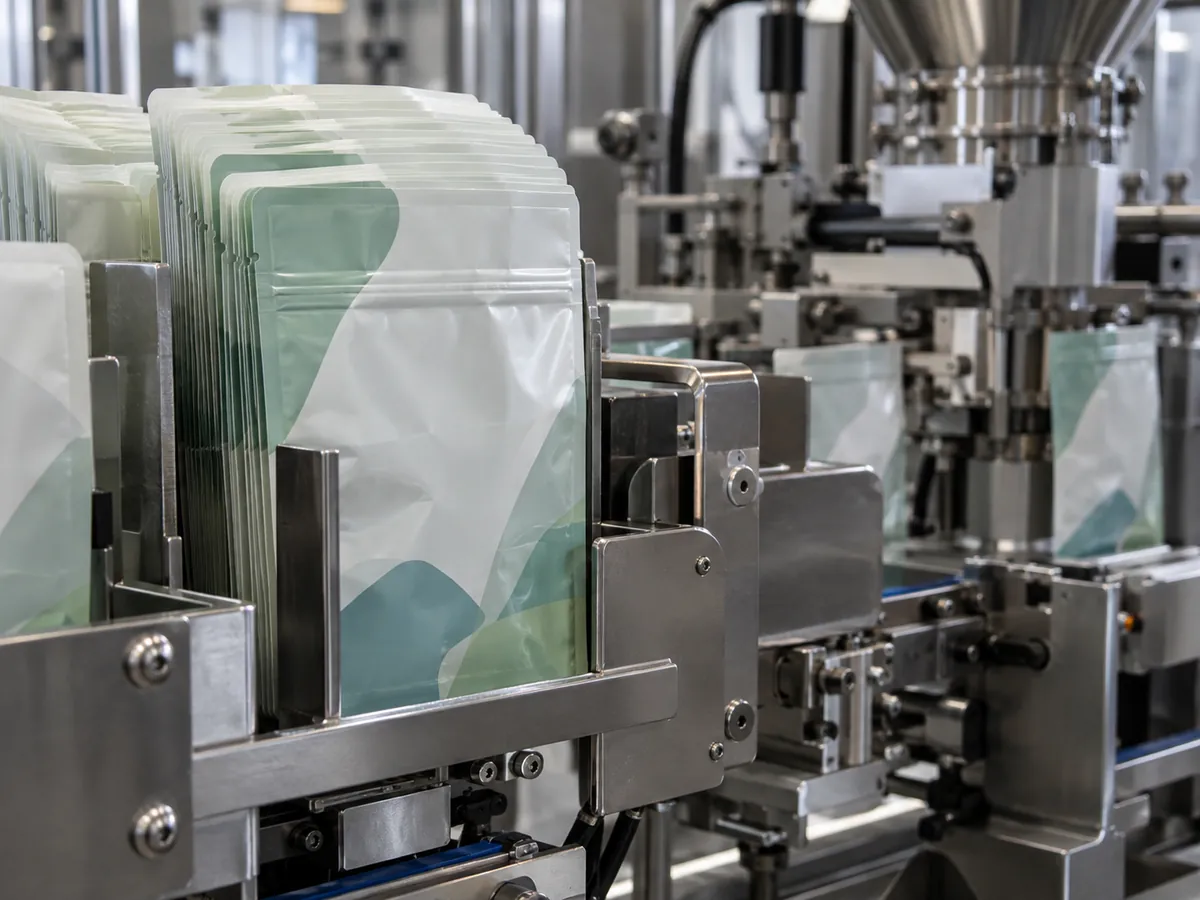
What the machine demands from the pouch
Dimensional tolerances and squareness
Width, height, seal width, bottom gusset depth and zipper position all need tolerances the machine can live with. A pouch that is out of square, curled or wider at one edge may jam in the magazine or arrive crooked at the grippers. Agree tolerances with the supplier in writing, and measure samples from several cartons rather than a single hand-picked sample. Even side seals and a consistent zipper distance from the top are common critical points. The format itself is covered in stand-up pouch.
Consistent stiffness
Panels need enough stiffness to hold their shape and open cleanly, but not so much that they resist the suction cups or crack at the gusset. Variation between lots matters more than the nominal figure. Thin, limp pouches may not open or may collapse around the filling tube. Very stiff ones can spring back or fail at fold points.
Sealant compatibility
The inner sealant has to seal in the machine’s dwell time and at its jaw temperature, with a window wide enough for drift. For a conventional top-filled pouch with a zipper below the final seal, check film-to-film sealing in the band above the zipper. Zipper-flange attachment to the panels and zipper-end/side-seal junctions are separate converter-made joints. Test those locations separately if the specified construction puts them at risk. Seal initiation temperature explains the first of these. A sealant that works on a form-fill-seal machine may not be right for a premade pouch machine because the geometry and dwell differ.
Clean seal areas
Dust, product residue and liquids in the seal area cause leaks. Two things control this: how the pouch is filled (the mouth must stay clear) and the sealant’s ability to seal through contamination. Fine powders, oils and sauces are a common source of leakers.
Zipper and spout specifications
Zipper width, profile, position and any tamper or slider features must suit the machine’s opening station and sealing jaws. Zipper ends can meet the side seals and need the converter’s specified termination treatment. This junction is distinct from a final top seal above the zipper. Other zipper locations, gussets and spout-filled designs need their own seal map. Spouts need dimension and orientation consistent with the feeder. Confirm zipper type and placement with the pouch machine builder, since opening devices are often tuned to a particular profile.
Static control
Static can make pouches cling together in the magazine, cause double picks and attract dust to the seal area. It tends to rise in dry conditions and with some film surfaces. Ask the supplier whether anti-static treatment is used, and check that it does not interfere with sealing or printing.
Bundling and supply
How pouches are bundled affects feeding. They may be supplied in cartons stacked flat, shingled or on a tray, with count and orientation specified. Excess handling at the converter or in transit deforms the stack. Specify carton size, count per bundle, orientation, any separator sheets, and how pallets are wrapped.
Rollstock (form-fill-seal) vs premade pouches
Scroll horizontally to view all columns if needed. ↔
| Factor | Rollstock form-fill-seal | Premade pouches |
|---|---|---|
| Format flexibility | Bag size set by machine tooling and film width | Pouch shape, gusset, zipper and spout can be varied |
| Pack appearance | Pillow or gusseted bags, fewer shapes | Stand-up shapes, zippers, spouts, shaped corners |
| Material cost per good pack | Record consumed rollstock and line losses | Record consumed pouches and filled rejects |
| Effective output | Measure at the selected bag/product conditions | Measure at the same bag/product conditions |
| Changeover | Film and format change, collar change | Pouch size change, gripper adjustment |
| Machine sensitivity | Film friction, tracking and hot tack | Pouch tolerances, stiffness, opening and final top-seal geometry |
| Supply risk | Roll quality, splices | Dimensional consistency, carton handling |
The choice depends on volume, product value and the pack appearance needed. VFFS film covers rollstock behavior, and the VFFS vs premade pouch comparison covers speed, footprint and operator skill in more depth.
Common problems and likely causes
Scroll horizontally to view all columns if needed. ↔
| Problem | Likely causes |
|---|---|
| Pouches not opening | Panels too stiff or too limp, static, suction cups worn or misadjusted, pouch mouth sealed from storage or heat, wrong air timing |
| Double picks | Static, pouches stuck together by pressure, excess slip or no slip, gripper vacuum too strong, poor stack presentation |
| Wrinkled top seals | Pouch not hanging square, jaw temperature or pressure outside window, mouth edges misaligned, product on the seal |
| Leaks near zipper | Identify flange, zipper-end/side joint or final top band first; inspect the responsible joint for inadequate bonding or contamination |
| Pouches out of square on the grippers | Dimension variation, curling from storage, bundle deformed, magazine mis-set |
What to put in a premade pouch specification
- Pouch style, dimensions and tolerances (width, height, gusset, seal widths) in writing.
- Film structure, sealant type and stiffness range.
- Seal initiation, seal window and hot tack data for the actual sealant.
- Zipper type, width, top-edge offset, flange attachment and end/side-seal treatment, separately from the final seal band.
- Spout or fitment size and orientation, where used.
- Static control and COF (ASTM D1894 is the test method).
- Bundle format, count per carton, orientation and pallet pattern.
- Printing and finishing: tear notches, hang holes, laser scores.
- Trial plan on the real machine with real product, and an agreed sample from each lot.
Confirm each item with the machine builder, because gripper design, opening method and jaw layout differ between models. For a first order, use the first-order risk checklist, and see packaging film machine compatibility for the wider view of machine requirements.
Method and sources
This is an editorial check framework, not a universal tolerance specification. One manufacturer’s 4SC-235 public sheet lists a 90–235 mm gripping range, 120–508 mm bag length and optional zipper opening/closing. Those are model-specific envelope dimensions, not pouch manufacturing tolerances; the page does not specify a zipper offset. Obtain the model’s approved pouch drawing for that input.
A pouch manufacturer’s bottom-filled tamper-evident pouch example lists top seal, zipper position and side seals separately. This example arrives sealed above its zipper and is filled through the bottom. It supports distinguishing seal locations and fill routes, not assuming another pouch shares its dimensions. Accessed 8 October 2026.
Continue reading
Related articles
Sachet Film: Choosing Packaging Film for Sachet Machines
Sachet packaging film runs on 3-side and 4-side seal machines. Compare structures, sealing, tear notches and fixes for leaks and seal-through-contamination.
Stick Pack Film: Materials and Machine Requirements for Stick Packs
Stick pack film is narrow laminate rollstock formed into slim tubes. See structures, sealing, lane slitting, tear notches, COF and machine checks.
VFFS Packaging Film: Materials, Sealing and Machine Compatibility Guide
VFFS film guide: common structures, thickness, barrier, sealing, COF, tracking and troubleshooting for vertical form fill seal machines and rollstock.