
Sachet Film: Choosing Packaging Film for Sachet Machines
Sachet packaging film runs on 3-side and 4-side seal machines. Compare structures, sealing, tear notches and fixes for leaks and seal-through-contamination.
Leaking sachets waste the dose, while film drag and unreliable sealing stop the line. Choose a structure against the actual product, contamination and barrier requirements, then test seals and opening on filled packs. This page covers the machine side; sachet packaging covers the format.
Product inputs before choosing film
Record the actual formulation and storage conditions before comparing structures.
Scroll horizontally to view all columns if needed. ↔
| Product / contamination | Compatibility and barrier inputs |
|---|---|
| Liquids (sauces, shampoo, sanitizer) | Sealant with good hot tack and tolerance for splashes. Compatibility with oils, alcohol or surfactants. Burst strength for drop and squeeze |
| Pastes and gels (creams, ketchup, toothpaste samples) | Contamination tolerance in the seal area, product adhesion to the sealant, easy squeeze-out |
| Fine powders (supplements, pharma, instant mixes) | Seal-through-dust, moisture barrier, static control, pinhole resistance |
| Granules (sugar, salt, detergent) | Abrasion and puncture resistance, strong seals at the pack corners |
| Aggressive products (essential oils, solvents, aggressive surfactants) | Chemical resistance of the sealant and adhesive, stress cracking in PE sealants. Test, because compatibility varies by formulation |
Where liquid or paste products carry fat or surfactant, the inner sealant can be attacked or the adhesive between layers can weaken. Ask for product compatibility testing on the real formulation, under agreed storage time and temperature conditions.
What sachet film does on the machine
A sachet machine pulls film from a reel, shapes it, seals the edges, fills the dose and seals the last edge. The film carries the print, protects the product and supplies the sealant surface. Sachets are small and run fast, so small variations in film behavior show up as leakers, skewed packs or stoppages.
Most sachet production runs on one of two machine types.
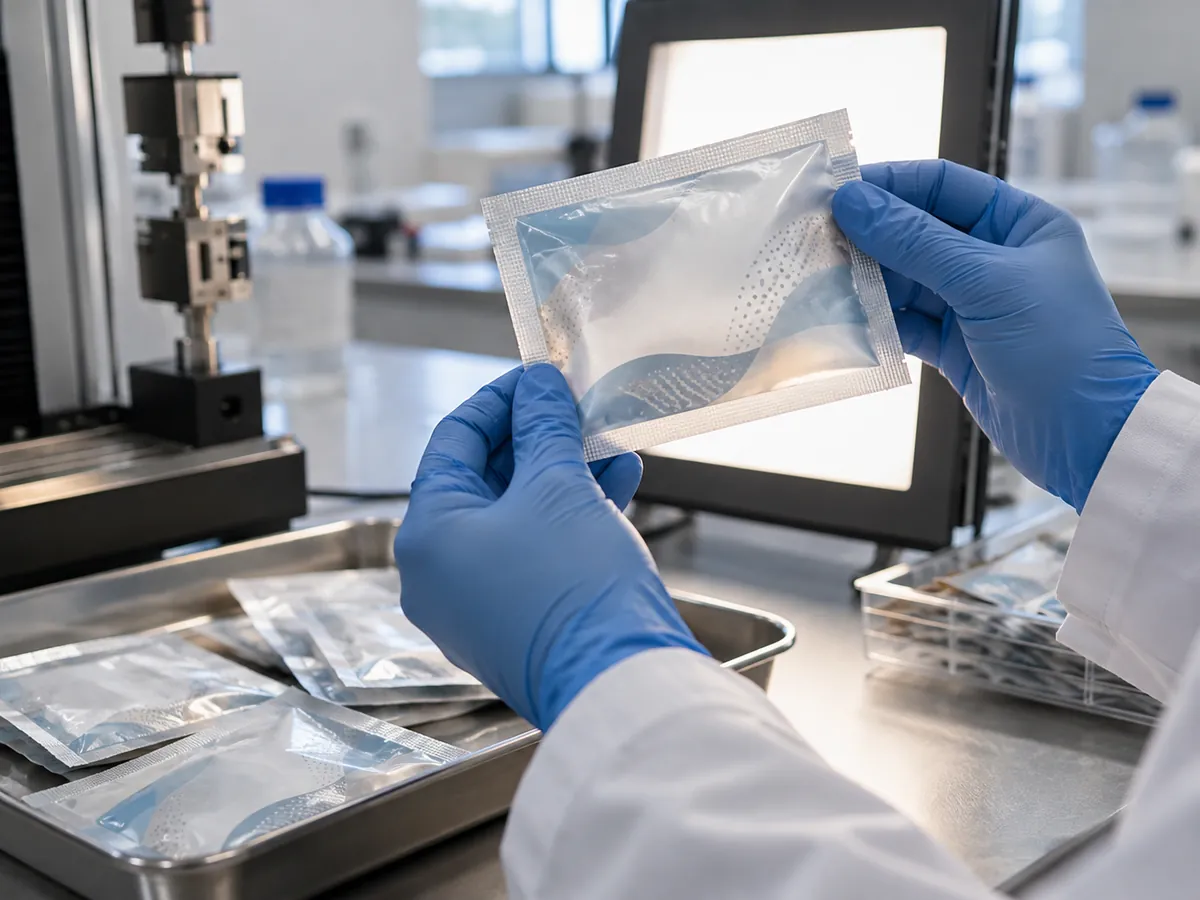
- 3-side seal: film is folded in half, either from a reel of single web or a pre-folded one. Two side seals and a top seal close the pack, and the fold forms the fourth edge. It is common for liquids, creams and powders.
- 4-side seal: two separate webs are sealed together on all four edges, so each side can use a different film, such as a clear side and a foil side. It is used for pharma powders, wipes and products that need a printed front and a barrier back.
Each can run as a single lane or as multi-lane, where a wide reel is slit and every lane makes its own sachets. On multi-lane machines, web flatness, even tension and slitting quality matter more, as covered for stick pack film.
Common sachet film structures
Scroll horizontally to view all columns if needed. ↔
| Structure | Typical use | Notes |
|---|---|---|
| PET/PE | Condiments, dry mixes, household samples | General purpose, printable, moderate barrier |
| PET/AL/PE | Pharma and nutrition powders, aggressive products, moisture-sensitive goods | Confirm finished-laminate oxygen, moisture and light protection, including defects and seals |
| PET/metPET/PE | Cosmetic samples, powders, cleaning products | Confirm barrier under the intended conditions; compare cost per accepted pack |
| Paper/PE or paper/AL/PE | Sugar, tea, wipes, natural look | Paper outer, check moisture handling and tear performance |
| BOPP/CPP or BOPP/metBOPP | Snack seasoning, condiments, dry goods | Good clarity or metal look, seals at moderate temperatures |
| Mono-PE | Designs aimed at PE recycling streams | Confirm structure-specific seal window, barrier and machine behavior |
For material details see PET film, aluminum foil and BOPP film.
Seal integrity and seal-through-contamination
Sachets have small seal areas and the product is often right at the seal. A pack can look sealed and still leak if product sits in the seal.
These are the parameters to check:
- Seal temperature, dwell and pressure: too cool gives weak seals, too hot gives distortion or burn-through. See seal initiation temperature.
- Hot tack: liquid or powder dropped into a warm seal can open it. Hot tack is commonly measured per ASTM F1921.
- Seal strength: commonly tested per ASTM F88. Test seals that have product in them as well as clean ones.
- Sealant type: some PE-based sealants are formulated to seal through light contamination. Ask the supplier which grade suits your product and jaw pattern.
- Jaw pattern: compare the installed jaw pattern with the machine guidance and trial clean and contaminated seals separately.
- Seal width: use the agreed seal drawing and test its tolerance to actual contamination.
Leak testing of finished sachets is commonly done with dye, vacuum or bubble methods. ASTM F2096 covers gross leak detection by internal pressurization (bubble test); validate its applicability to the actual package. A seal-strength result does not substitute for leakage testing, and a leak test does not measure peel strength.
Tear notches and easy opening
A notch starts an opening; it does not establish the tear path of the whole laminate. Do not infer straight tearing from “PET” or “BOPP” alone. Record layer structure, orientation, thickness and notch/score position. A converter’s public laser-scoring guidance supports machine- and cross-direction scoring with settings chosen for different materials, not a universal tear direction.
Test filled packs in the intended opening direction after the agreed storage and temperature/humidity conditioning. Record whether the tear follows the intended path, opens the dose cleanly and leaves the product accessible. Confirm the scored pack still meets its barrier and integrity criteria.
COF, tracking and registration
Coefficient of friction controls how film runs over forming plates or collars and through the feed. Too high gives drag and wrinkles. Too low gives slipping on the rollers and variable pack length. ASTM D1894 is the usual test method; see coefficient of friction. Registration marks need good contrast against the background, and sensor settings must suit metallized or dark films.
Common sachet problems
Scroll horizontally to view all columns if needed. ↔
| Problem | Likely causes |
|---|---|
| Leaking sachets | Product in the seal, low hot tack, wrong temperature, worn or misaligned jaws |
| Weak seals | Temperature or dwell too low, sealant not suited to the product, contamination |
| Burn-through or distorted seals | Temperature too high, dwell too long, film too thin for the structure |
| Wrinkles at seals | High COF, uneven tension, poor web guiding |
| Tear fails or goes crooked | Notch misplaced, structure unsuited to hand tearing |
| Pack length variation | Slipping at feed rollers, stretch in the film, sensor misreading marks |
| Product attacks the film | Sealant or adhesive not compatible with the formulation |
Sachet specification and trial record
Copy this record for each material batch and trial condition; agree criteria before running a full-roll trial with the real product.
Scroll horizontally to view all columns if needed. ↔
| Field | Planned input / acceptance basis | Actual result / evidence |
|---|---|---|
| Product / format | Formulation, dose, 3/4-side layout and lanes: ___ | Batch and sample IDs: ___ |
| Film / roll | Structure, gauge, width, core, unwind: ___ | Machine/model and fit result: ___ |
| Barrier / compatibility | OTR, WVTR, method and conditioning: ___ | Report / storage evaluation: ___ |
| Sealing | Temperature, dwell, pressure and contamination: ___ | Actual settings; hot-tack/strength and leak results, separately: ___ |
| Handling / opening | COF faces, notch/score, tear direction and criteria: ___ | Tracking, opening results, stopped minutes and reject count: ___ |
| Release | Owner and acceptance document: ___ | Accept/hold, approver and date: ___ |
For the wider picture, read packaging film and machine compatibility.
Method and sources
The input and record tables are editorial suggestions. Public scopes checked 8 October 2026: ASTM F88/F88M-23, force to separate a seal specimen; F1921/F1921M-12(2023), instrumented hot seal strength; F2096-11(2019), gross leaks; D1894-24, starting/sliding friction under specified conditions. These scopes supply no project acceptance limits. A converter’s slitting and laser-scoring documentation describes directional scoring and material-dependent settings; it does not certify this page’s candidate structures.
Continue reading
Related articles
Premade Pouch Packaging Materials: What Pouch Machines Need
Premade pouch packaging materials explained: tolerances, stiffness, sealants, zippers and the specs pouch machines need to open, fill and seal reliably.
Stick Pack Film: Materials and Machine Requirements for Stick Packs
Stick pack film is narrow laminate rollstock formed into slim tubes. See structures, sealing, lane slitting, tear notches, COF and machine checks.
VFFS Packaging Film: Materials, Sealing and Machine Compatibility Guide
VFFS film guide: common structures, thickness, barrier, sealing, COF, tracking and troubleshooting for vertical form fill seal machines and rollstock.