
Stick Pack Film: Materials and Machine Requirements for Stick Packs
Stick pack film is narrow laminate rollstock formed into slim tubes. See structures, sealing, lane slitting, tear notches, COF and machine checks.
Stick pack film is rollstock formed into narrow tubes with a longitudinal fin or lap seal and cross-sealed ends. On a multi-lane line, a film that works on one tube can still cause leaks or stoppages on other lanes. Confirm the five inputs below before ordering; the finished format is covered in stick pack packaging.
Scroll horizontally to view all columns if needed. ↔
| Input | Record from the actual machine/product |
|---|---|
| Lane pitch | Tube/slitter layout and drawing revision |
| Single-lane strip width | Width and tolerance for the installed tube and fin/lap geometry |
| Full roll width | Slitter layout, edge trim and permitted reel width |
| Longitudinal seal type | Fin: inner-to-inner; lap: overlapping inner-to-outer, with compatible surfaces |
| Product dust | Actual product, dose and contamination observed at each seal |
What stick pack film is
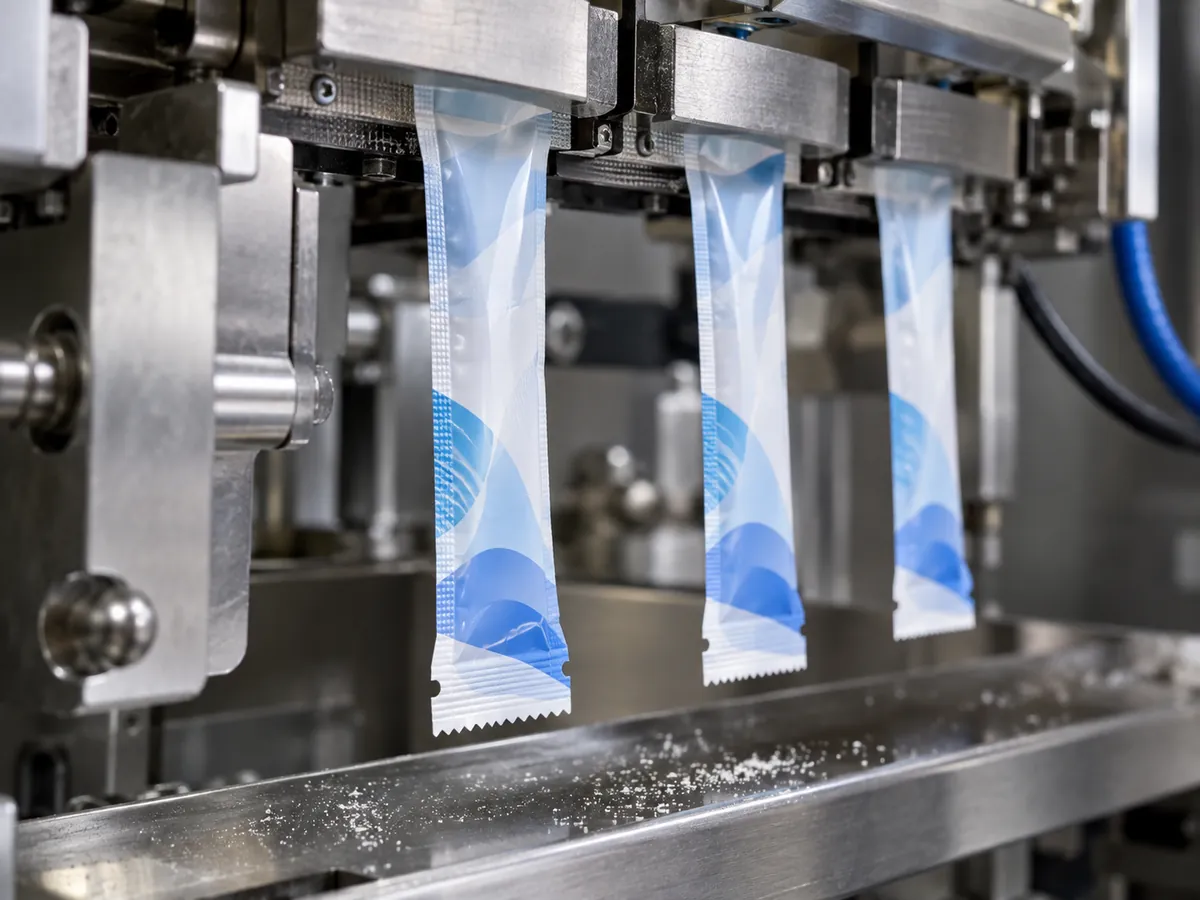
A stick pack machine works like a very small vertical form fill seal machine. Film unwinds from a reel, is guided over a forming tube, and the edges are joined by a fin seal (inside faces sealed together) or sometimes a lap seal. A dosing unit drops powder, granules or liquid down the tube. Cross-sealing jaws then close the bottom of one stick and the top of the next, and a knife separates them. The same principles apply as on VFFS film, but at a much smaller scale and with tighter tolerances.
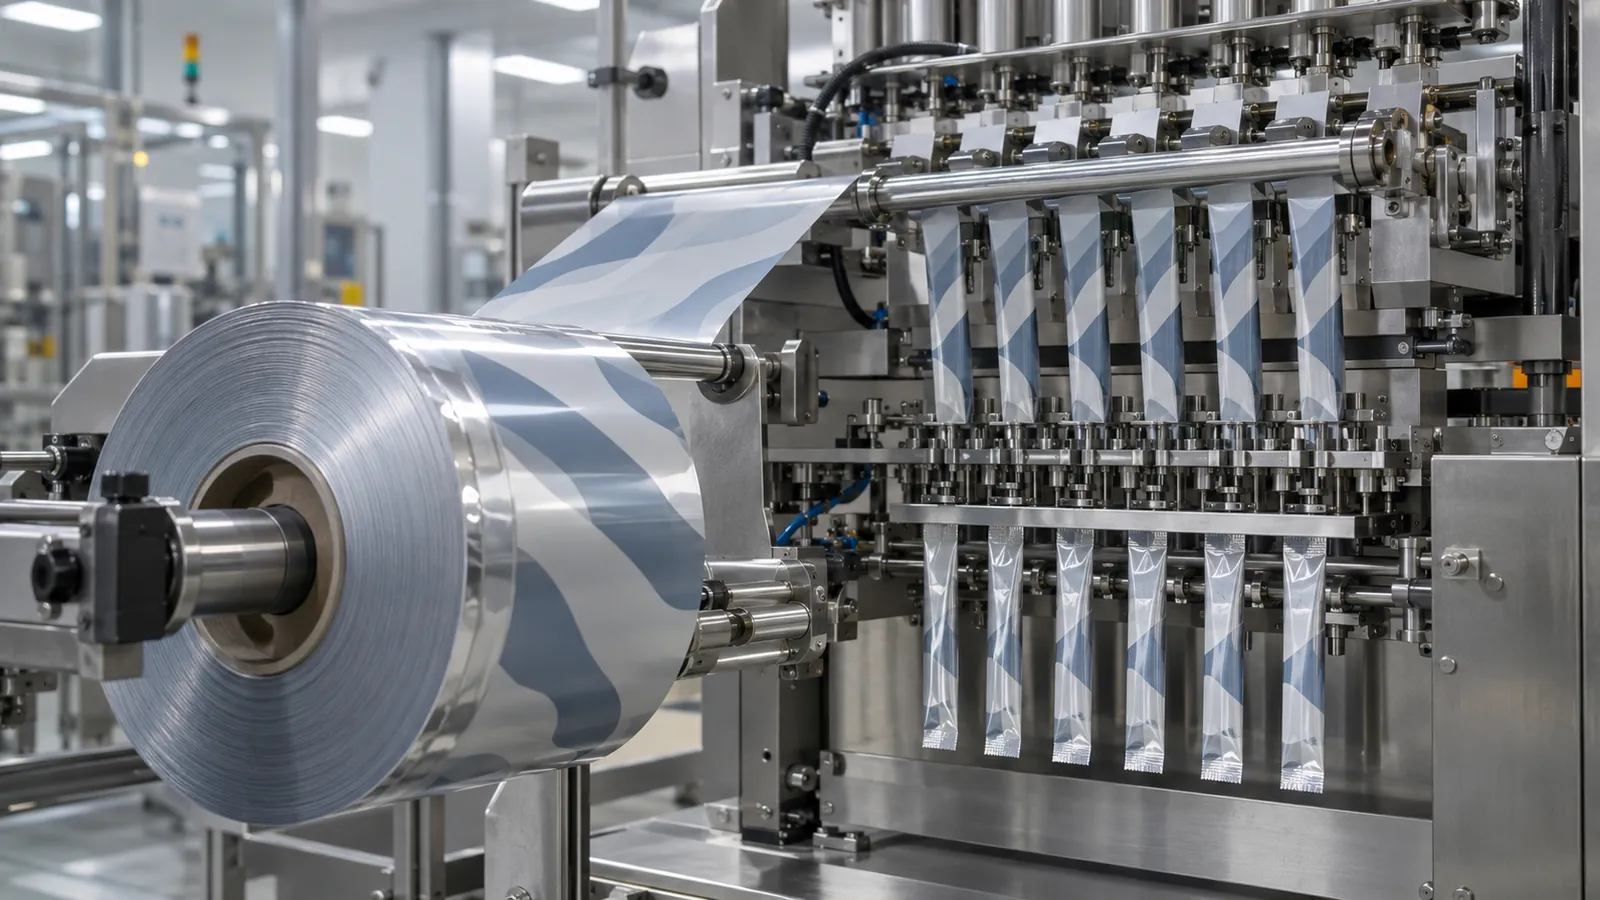
On a multi-lane machine the web is wide, often slit into narrow ribbons on the machine itself, and each ribbon forms its own tube. A film that runs well at one lane in the lab can behave differently when multiple lanes share tension controls or sealing hardware.
Stick pack packaging material usually means the whole structure: print layer, optional barrier layer and an inner sealant layer.
Confirm the actual stick pack structure
Do not approve a laminate from its layer names or the product category alone. Record the complete structure, gauge, strip width and product alongside the converter’s current technical sheet and filled-pack trial. A machine process description supports how the web forms and seals; it does not certify PET/AL/PE, paper laminates, metallized films or mono-PE for your shelf life.
Scroll horizontally to view all columns if needed. ↔
| Structure / gauge | Strip width / lane layout | Product / dose | Barrier and seal evidence | Source / revision / date | Accepted trial |
|---|---|---|---|---|---|
| ___ | ___ | ___ | ___ | ___ | ___ |
Material background is in aluminum foil and PET film. Confirm recycling claims against the destination system and the finished design; mono-material packaging explains that separate decision.
Film thickness
Use the actual laminate’s gauge and tolerance against the installed machine’s approved range. There is no sourced universal thickness range here. Record the transverse gauge profile as well as nominal thickness, then check forming, longitudinal seals and end seals on every active lane at the planned operating conditions.
Multi-lane machines and slitting the web
Confirm the lane count and film feed arrangement on the installed model. Film can reach the forming tubes in these arrangements:
- Wide reel slit on the machine: the reel is as wide as all lanes together, and slitter knives on the machine cut it into ribbons before forming. Edge quality matters, because dust, burrs or edge fuzz from slitting can contaminate seals.
- Pre-slit narrow reels: use only where the machine provides the matching unwind arrangement; record reel-change time rather than assuming it.
For either method, check these:
- Width tolerance: check each strip against its forming-tube drawing and confirm the combined slitter layout.
- Roll build: uniform tension and flat winding across the width stop some lanes pulling slack while others are tight. Telescoping or gauge bands show up first at the edge lanes.
- Gauge profile: variation across the web changes seal quality lane by lane.
Fin seal, back seal and cross seals
The longitudinal or back seal can use different geometries. A manufacturer’s public process description shows a wide web passing through a slitter, then each strip passing over its own forming tube before longitudinal and cross sealing.
Scroll horizontally to view all columns if needed. ↔
| Stage / seal | Geometry to check on the drawing | Consequence for film width |
|---|---|---|
| Slitting | Full web → individual strips → one forming tube per lane | Confirm strip widths, edge trim and alignment; lane pitch alone is not the strip-width specification |
| Fin seal | Inner faces of both strip edges meet; seam projects from the tube | Drawing needs film allowance for both projecting edges |
| Lap seal | One edge overlaps the other; inner face contacts the outer face | Confirm overlap allowance and outer-surface seal compatibility; do not reuse the fin-seal width |
| Cross seals | Jaws close each tube at its ends | Check contamination, seal alignment and opening on every lane |
The public description states that its lap arrangement uses less film than its fin arrangement. It gives no universal width saving; obtain the actual forming and seal drawing. No numerical width example is assumed here.
Ask for the seal window on the finished structure. Seal initiation temperature explains that input. ASTM F1921/F1921M covers hot-tack measurements before cooling; ASTM F88/F88M covers seal-specimen strength. Neither supplies a universal machine setting or replaces a filled-pack leak check.
Sealing through dust and powders
With a powder product, record contamination at the longitudinal and end seals lane by lane. Compare clean and product-exposed seals using the actual laminate. Confirm whether the dosing arrangement, extraction or sealant grade controls the observed contamination; do not assume a serrated jaw or a PE-based sealant can seal through any amount of dust.
Scroll horizontally to view all columns if needed. ↔
| Run / batch / speed | Lane ID / strip width | Longitudinal seal result | End-seal leak result | Dust / wrinkle / cut defect | Changed setting | Evidence / disposition |
|---|---|---|---|---|---|---|
| ___ | ___ | ___ | ___ | ___ | ___ | ___ |
Repeat the row for every lane and record sample count and acceptance criteria. A single-lane success does not release the full-width web: compare lane tension, cut edges, gauge profile and contamination before changing shared settings.
Tear notches and easy opening
Specify the required hand-opening method and the actual notch or score geometry. Layer names such as PET or BOPP do not establish the tear path of the finished laminate. Test its orientation, bond and tear-start design together. Hand-opening should be tested on filled packs, including at the temperatures and humidity the product will meet, because tear behavior changes with moisture and temperature.
COF and tracking across lanes
Coefficient of friction controls how film pulls over the forming tubes and through the pull-down. On a multi-lane machine, even small differences between lanes add up, because one pull-down system moves every lane together. If friction against metal is too high, lanes drag unevenly and tubes wrinkle. If too low, the film slips on the belts and stick length varies. ASTM D1894-24 measures starting and sliding friction against a specified surface; its scope notes sensitivity to film age and additive bloom. Record surface, conditioning and age instead of treating a single COF value as a machine pass limit. More in coefficient of friction.
Tracking across many lanes depends on a flat, evenly tensioned web. Wavy edges, slack lanes and curl turn into skewed packs and misaligned seals.
Registration
Printed sticks rely on a registration mark read per lane or across the web. Metallized or dark backgrounds can reduce mark contrast. Print repeat must match pack length, and tension should stay stable from roll start to finish, because stretch moves the mark and the cut.
Common stick pack problems
Scroll horizontally to view all columns if needed. ↔
| Problem | Likely causes |
|---|---|
| Leaking sticks | Powder in the seal, low hot tack, wrong jaw temperature, worn jaw faces |
| Wrinkles on the tube | COF too high, film too thin, uneven tension, worn forming tube |
| Lane-to-lane variation in length | Uneven film tension, low COF on the belts, slitting width errors |
| Tear fails or runs crooked | Notch misplaced, film not suited to tearing, foil layer or laminate bond issue |
| Fin seal opens | Contamination or low temperature at the back seal, mismatch between sealant and jaw |
| Print misregistration | Stretch, mark contrast, repeat length mismatch |
What to put in a stick pack film specification
- Define the product (powder, granule, liquid, gel), dose weight and stick dimensions.
- Set barrier needs (oxygen, moisture, light, aroma) with test conditions and shelf life. See OTR and WVTR.
- Match the finished structure to measured barrier and sealing requirements, using its dated technical sheet.
- Ask for seal window and hot tack curves of the sealant on the real structure.
- Specify COF inside and outside, with test method.
- Define tear method, notch position and the opening force you want.
- Confirm roll width, core, outer diameter, weight, lane count and slitting method.
- Define registration mark size, position and contrast.
- Run a full-roll trial at target speed with real product, and test filled sticks for leaks and tear.
What to confirm with the machine builder
- Lane count and lane pitch: these set reel width and slitter layout.
- Forming tube size: matched to the stick width.
- Jaw type and pattern: constant heat or impulse, plain or serrated, and notching or scoring tooling.
- Reel limits: maximum roll width, outer diameter, weight, core size and unwind direction.
- Registration and sensors: sensor type, mark color and size.
Related resources
- StickPackMachine.net: a related machine-resource site in this publishing network, linked for format background. This is not an independent supplier recommendation, a film acceptance source or an enquiry service offered by this site.
Sources and method
Checked 8 October 2026. Records above are editorial worksheets, not measured results.
- Viking Masek, “How do Stick Pack Machines Work?”, 26 April 2018: manufacturer’s public account of slitting, one forming tube per strip, fin/lap geometry and filling/sealing. It does not validate a general film gauge or a specific laminate/product pairing.
- ASTM F1921/F1921M-12(2023), F88/F88M-23 and D1894-24: official method scopes for hot tack, seal strength and friction. Project acceptance limits remain inputs.
Continue reading
Related articles
Premade Pouch Packaging Materials: What Pouch Machines Need
Premade pouch packaging materials explained: tolerances, stiffness, sealants, zippers and the specs pouch machines need to open, fill and seal reliably.
Sachet Film: Choosing Packaging Film for Sachet Machines
Sachet packaging film runs on 3-side and 4-side seal machines. Compare structures, sealing, tear notches and fixes for leaks and seal-through-contamination.
VFFS Packaging Film: Materials, Sealing and Machine Compatibility Guide
VFFS film guide: common structures, thickness, barrier, sealing, COF, tracking and troubleshooting for vertical form fill seal machines and rollstock.