
Medical Device Packaging Materials: Sterile Barrier Systems Explained
Medical device packaging materials form the sterile barrier: breathable paper or nonwoven, peel pouches, trays and lidding. See how sterilization drives choices.
An incompatible sterilization cycle can damage a package intended to maintain a sterile barrier. Select the cycle and grade-specific packaging system together, then validate seals and integrity through aging and distribution.
Scroll horizontally to view all columns if needed. ↔
| Method | Candidate barrier component | Grade / validation gate |
|---|---|---|
| Ethylene oxide (EO) | Gas-permeable medical paper or documented nonwoven component | Confirm sterilant access, aeration, seal and microbial-barrier performance |
| Gamma / electron beam | Documented radiation-compatible film, paper or nonwoven system | Confirm dose range, material change and seals after aging |
| Steam | Cycle-qualified permeable web plus compatible film / tray | Confirm grade, heat/moisture tolerance and integrity; HDPE family name is insufficient |
This matrix is an entry point, not a sterilization approval. Obtain the supplier’s grade/cycle documentation and validate the assembled system.
ISO 11607 and the sterile barrier system
ISO 11607 is the standard framework for packaging of terminally sterilized medical devices. It splits the job into two parts: requirements for materials and preformed systems (such as pouches and trays), and requirements for validating the forming, sealing and assembly process. It also uses a few terms worth knowing:
- Sterile barrier system: the minimum package that prevents microbial ingress and allows aseptic presentation at the point of use. A sealed pouch is one example.
- Protective packaging: extra packaging, such as a carton or an outer pouch, that protects the sterile barrier system in handling and distribution.
- Packaging system: the sterile barrier system plus protective packaging.
ISO 11607-1:2019 covers materials, sterile barrier systems and packaging systems. ISO 11607-2:2019 covers forming, sealing and assembly validation; both have a 2023 risk-management amendment. Check the destination regulator’s recognized edition and extent of recognition separately from the publisher’s catalog, for example in the FDA recognition database. This page summarizes public scopes, not the full compliance requirements.
Sterilization method drives material choice
Sterilants reach the device in different ways, and that decides which materials can sit in the package wall.
Ethylene oxide
Ethylene oxide is a gas. It has to get in through the package, act on the device, and then be removed again during aeration, so at least one component of the barrier must be gas permeable while still blocking microorganisms. Medical-grade paper and spunbonded nonwoven made of high-density polyethylene are the usual breathable components. A fully sealed film and foil pouch is generally not suitable for this method.
Gamma and electron beam radiation
Radiation passes through the package, so breathability is not needed. The concern is what radiation does to the polymers. Gamma and e-beam exposure can cause discoloration, embrittlement, odor or changes in seal behavior in some plastics, and effects can continue to develop after exposure. Test materials at the dose range you plan to use, including after aging. Some polymers cope well and others do not, so confirm with the supplier and your own data.
Steam
Steam sterilization combines heat, pressure and moisture. Materials must tolerate the temperature, and the package must let steam in and air out. Use a permeable web and mating film documented for the exact steam cycle; generic paper or nonwoven selection does not establish compatibility. Heat-sensitive peel films may not be suitable.
Other methods exist, including hydrogen peroxide gas plasma and, for some products, other low-temperature processes. The same rule applies: the sterilant must reach the device through the barrier, and nothing in the package may be damaged or leave residues that matter.
Breathable materials
Medical-grade paper
Medical-grade paper is a porous sheet made for sterilization packaging. It lets gases through while filtering out microorganisms. It is often coated with a heat-seal layer on the side that meets the film. Fiber tear on opening is a known behavior, and good grades are specified for low particle release. Paper is generally less strong when wet and less puncture resistant than a nonwoven.
Spunbonded HDPE nonwoven
This is a nonwoven sheet made from fine high-density polyethylene fibers, bonded without a binder. It is strong, tear and puncture resistant, and resists moisture, so it is often chosen for heavier or sharper devices. It is breathable enough for ethylene oxide and is used in both pouches and lidding. Not every grade tolerates a given steam cycle. A nonwoven manufacturer publishes compatibility only under controlled steam conditions; confirm the exact grade, coating, mating film and cycle rather than extending that statement to all HDPE nonwovens. HDPE film and PE packaging film give general film background.
Package types
Peel pouches and header bags
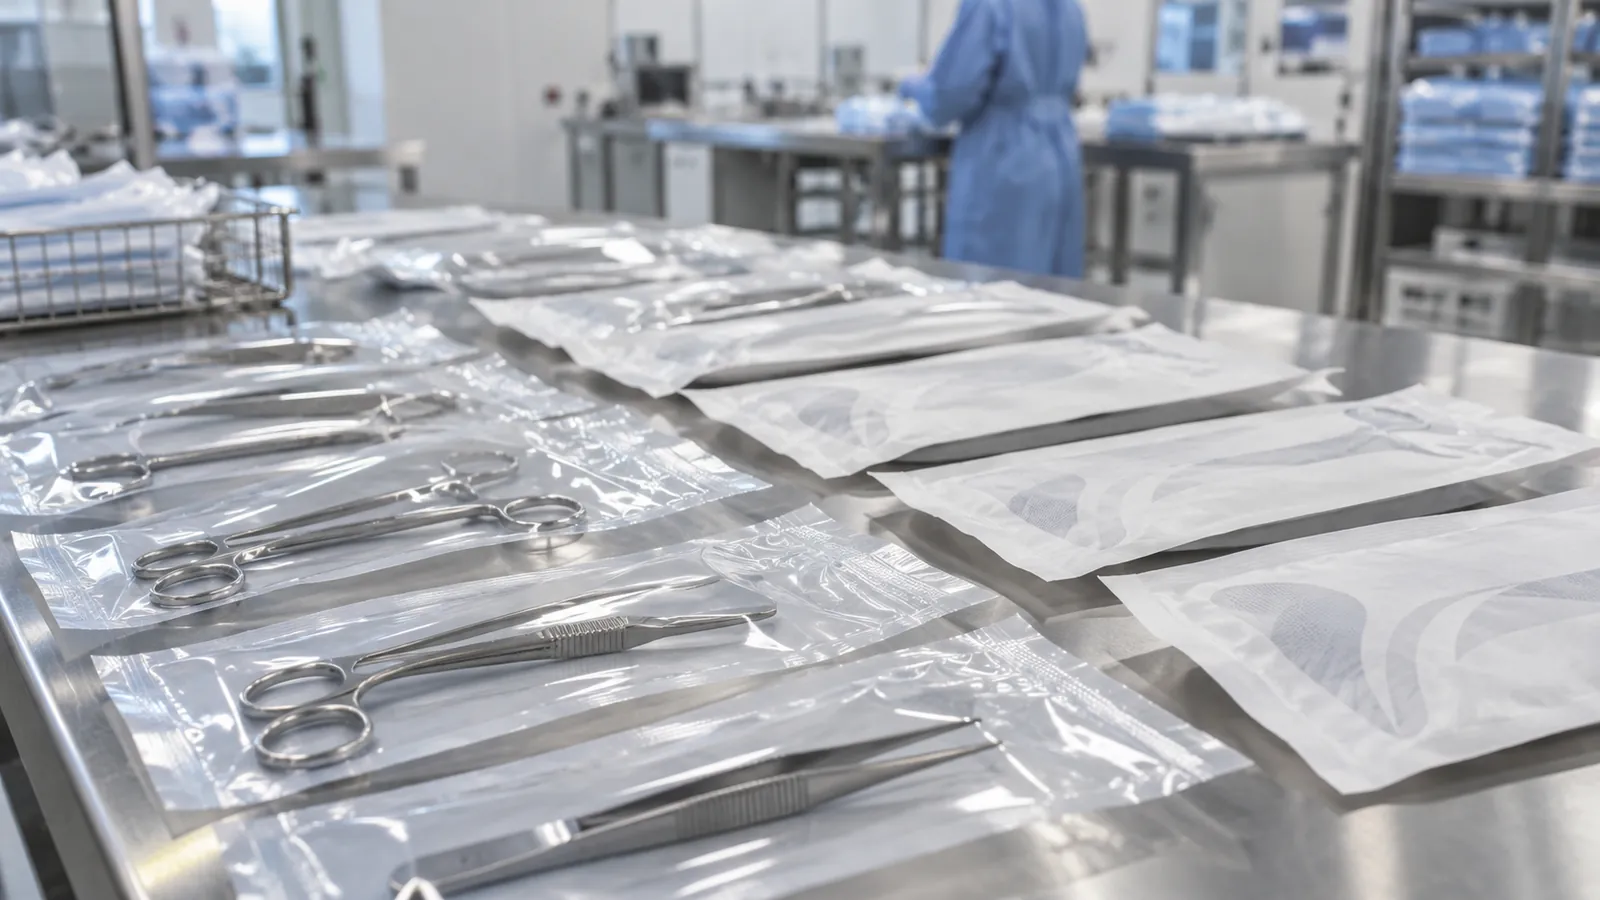
A peel pouch pairs a transparent film with a breathable paper or nonwoven web, sealed around the edges. The film is often a laminate such as polyester with a heat-seal layer, so the user sees the device and can peel the two faces apart. Header bags are similar but have a breathable header, a strip of paper or nonwoven sealed across the top of an otherwise film bag. Fully film pouches (with no breathable face) suit radiation sterilization where breathability is not needed. Premade pouch materials covers the format side.
Thermoformed trays with lidding
Rigid or semi-rigid trays hold devices that need positioning or protection, such as implants, kits and instruments. Trays are thermoformed from materials like PETG or other polymers, then sealed with a lid of breathable nonwoven or paper, or a film or foil lid when breathability is not needed. The lid’s heat-seal coating must match the tray polymer. Lidding foil explains coated lids in general.
Peelability and fiber tear
A sterile barrier must open without damaging the device or contaminating the field. Two behaviors matter.
- Peel: the seal separates cleanly at its interface, ideally with a steady force and no stringing or film residue left on the device side.
- Fiber tear: the paper or nonwoven delaminates at the seal and leaves fibers on the film. Excessive fiber tear is a defect on many specifications because loose fibers could reach the sterile field. It also indicates the seal is stronger than the sheet.
Seal strength has to sit in a window: strong enough to survive distribution and weak enough to open without force. Packaging seal strength covers the general concept.
Seal integrity and package testing
Typical checks cover both the seals and the finished packages.
Scroll horizontally to view all columns if needed. ↔
| Test | What it tells you | Common reference |
|---|---|---|
| Seal strength (peel) | Force to separate a sampled seal | ASTM F88/F88M-23 |
| Gross leak by bubble test | Gross leaks under specified internal pressurization; confirm method suitability for the web | ASTM F2096-11(2019) |
| Visual seal inspection | Channels, wrinkles, voids, incomplete seal | Visual, often with dye or other methods |
| Distribution and aging studies | Whether the package still works after transport and shelf life | Defined in the validation plan |
ASTM F88 measures how much force it takes to pull a seal apart. ASTM F2096 detects gross leaks by submerging the package, pressurizing it internally and watching for bubbles. Neither on its own proves sterility. ISO 11607 expects validation of the sealing process, including installation, operation and performance qualification, plus routine monitoring.
Device and pharmaceutical packaging boundaries
Terminally sterilized device packaging and drug container systems require different assessments; ISO 11607-1 also notes additional requirements may apply to drug/device combinations. Pharmaceutical flexible packaging covers the drug formats; pharmaceutical flow wrap explains that package format without approving it as a sterile barrier.
Steps to specify a sterile barrier package
Scroll horizontally to view all columns if needed. ↔
| Check | Record for each sample / time point | Result / action |
|---|---|---|
| Protocol / traceability | Device, material / coating lots, cycle and dose; methods / versions; acceptance criteria | Resolve missing grade/cycle documentation |
| Before / after sterilization | Matched sample sets; peel, failure mode, visual and integrity results | Investigate change from baseline |
| After aging | Time / conditions; peel, channel, microbial-barrier and integrity assessments in plan | Hold failed configuration |
| After distribution | Transport sequence / conditions; device damage, seal and barrier results | Compare with predefined criteria |
| Change control | Grade, coating, fiber, equipment or cycle changes; affected validation records | Review before releasing changed system |
Seal strength is not a sterility test
F88 measures separation force from a seal specimen; it does not test microbial ingress or every part of the finished package. F2096 addresses gross leaks and has material-suitability limits in its public scope. Combine qualified integrity methods with sterilization and packaging-process validation; neither test alone proves sterility.
For follow-up, use seal strength and integrity checks and film specification comparison to organize method and supplier documents.
Method and sources
Edition information and scope were checked in official catalogs; full paid standards and destination-specific recognition assessments are outside this introduction. Manufacturer compatibility is a conditional statement, not our testing. Official catalogs and the steam-compatibility notice reviewed 2026-10-08; no sterile-barrier validation is performed here.
Continue reading
Related articles
Spice Packaging Materials: Aroma, Moisture and Contact-Layer Checks
The best spice packaging depends on whole or ground form, climate and how spice oils meet the inner layer. Compare the risks, then copy a sample record.
Bakery Packaging Film: Keeping Bread and Cakes Fresh
Bakery packaging film explained: how staling, moisture loss and mold shape film choice for bread, cakes, cookies and tortillas, plus formats and machines.
Cheese Packaging Film: Ripening, Vacuum and MAP
Cheese packaging film explained: gas-permeable ripening films, vacuum bags for blocks, MAP for sliced and shredded cheese, reclosable packs and structures.