
Mono PE vs Multilayer Film: Recyclability vs Performance
Mono PE vs mixed-material multilayer film compared on recyclability, barrier, seal window, print and cost, with guidance on which structure suits your product and line.
Switching film without checking shelf life and line yield can lose more than it saves. Mono PE film is a polyethylene-based structure, not necessarily a single layer: it is often itself multilayer, with an oriented PE outer web, a PE sealant and sometimes a coextruded core. Recycling design guidelines such as CEFLEX’s allow limited amounts of non-PE barrier layers, coatings, adhesives and inks within set thresholds, so a pack built to those limits can go into a PE recycling stream where one exists. Multilayer film in this comparison means a mixed-material laminate such as PET/PE or PET/foil/PE, which combines different polymers or foil for print, barrier and sealing. Consider a PE-based candidate when the recycling target, product protection and line trial can all be met. Retain the qualified mixed-material pack until the replacement meets its shelf-life and seal-integrity requirements. This comparison organizes public guidance; it is not a test by this site.
For background, see mono-PE packaging, mono-material packaging and laminated packaging.
Mono PE vs mixed-material multilayer film at a glance
Compare specified structures rather than grouping PET/PE and PET/foil/PE as one barrier grade. No shared thickness or test dataset supports fixed performance rankings here.
Scroll horizontally to view all columns if needed. ↔
| Comparison input | Record for both candidates |
|---|---|
| Layer build | PE-based outer/bond/sealant, with any barrier; versus exact PET/PE or PET/foil/PE build |
| Thickness | Each layer and total gauge, from the grade-specific specification; not supplied here |
| Intended use | Same product, fill, shelf-life target and storage/distribution |
| Barrier | OTR/WVTR, method, temperature/RH and post-conversion condition |
| Sealing | Machine, speed, temperature/dwell/pressure, hot tack and integrity |
| Mechanical/print | Grade, MD/TD method and conditioning; trial registration |
| Recycling | Full-pack assessment under destination protocol/version |
CEFLEX supports a design preference for mono-polyolefin structures over mixed materials. It does not establish a universal barrier, optics or sealing winner; supplier results need the conditions above.
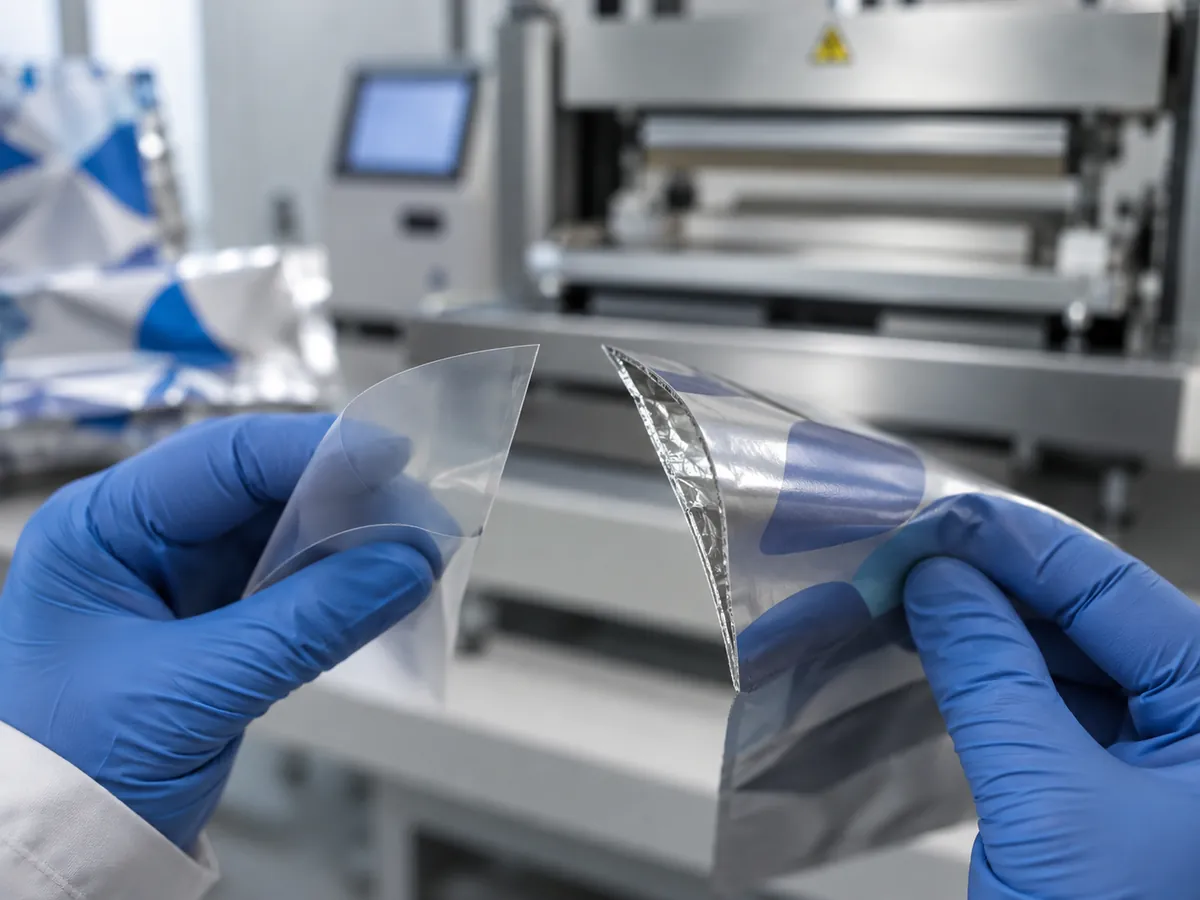
Recyclability: the case for mono PE
Collection and sorting systems struggle to separate the layers of a PET/PE laminate. A mono PE structure keeps the outer web, sealant and most other layers in one polymer family, so a pack that meets a design guideline is recyclable in principle. Guidelines from CEFLEX, RecyClass and APR set limits on barrier layers, inks, adhesives and fitments. They are updated from time to time, so check the version you design to.
Two cautions apply. First, recyclable in principle is not the same as recycled in practice, because whether PE film is collected and sorted depends on where the pack is sold. Second, regulation is changing what buyers expect in some markets. Recyclable flexible packaging and design for recycling explain how claims and checks work.
Compare barrier and sealing results
A PET/PE laminate and a PET/foil/PE laminate are different barrier candidates. A PE-based structure may contain a permitted barrier layer or coating. Compare OTR and WVTR at matching test temperature and relative humidity, then verify the converted pack against the product’s shelf-life target.
Likewise, qualify the actual seal window instead of assigning “wide” or “narrow” from the label. Check outer-web distortion and sticking alongside hot tack, cooled strength and integrity.
Takeaway: Retain the established pack if the replacement cannot meet its documented protection and sealing requirements.
Line and machine considerations
Moving from a laminate to mono PE takes a trial. It is not a straight film swap.
- Build a seal curve for the actual structure. A PET/PE starting point may not carry over.
- Check jaw temperature uniformity; small differences matter in a narrow window.
- Watch dwell, pressure and temperature together. On VFFS lines, test hot tack.
- Check stiffness over the forming collar, and check tracking. A softer outer film can behave differently from PET, as the page on VFFS film explains.
- Test seals at the edges of the running window as well as the center, and run long trials with stops and restarts.
Takeaway: Use the qualified current pack as the line baseline; measure the candidate through the same run, stop and restart conditions.
Print, lamination and cost
Oriented PE films can be reverse printed, but they are less dimensionally stable than PET under web tension and drying heat, so registration and tension control need care. Adhesives and inks are part of the recycling assessment, so ask for the adhesive type and coat weight, and keep ink coverage to what the design needs.
No general rule applies to cost. Film prices, barrier layers, converter yield, line speed changes and trial time all vary, and a cheaper film can cost more on the line. Compare on total cost per good pack.
Product fit
Dry, frozen and oxygen-sensitive products are trial contexts, not automatic passes or exclusions. Set the product’s barrier, mechanical and storage needs before choosing either route. For a retort project, use retort-pouch qualification rather than this general comparison.
Takeaway: A candidate that cannot meet the actual product exposure or shelf-life target is unsuitable regardless of its recycling label.
When to choose mono PE
Start a PE-based trial when a destination recycling target exists, the full pack can be assessed against it and you have a product-protection target and trial capacity. A successful material assessment alone does not approve the filling-line settings.
Takeaway: Proceed only when barrier, process yield and finished-pack integrity are qualified as well.
When to choose a multilayer film
Keep the qualified mixed-material laminate when the proposed replacement lacks matching barrier data, fails the shelf-life study or cannot sustain the needed seal integrity and line yield. A recycling objective does not resolve those failures.
Common mistake: Rejecting every PE-based option or approving every one from the polymer label alone.
Takeaway: Decide on the documented structure and results, not a category-wide ranking.
Questions to answer before switching to mono PE
Complete this assessment for the current and proposed packs. Unknown critical results mean the replacement remains unqualified.
Scroll horizontally to view all columns if needed. ↔
| Assessment field | Answer / evidence to fill in |
|---|---|
| Recycling guideline, version and region | ___ |
| Product OTR/WVTR and shelf-life targets | ___; methods and conditions: ___ |
| Candidate barrier and shelf-life study | ___; meets target? ___ |
| Collection/sorting route at destination | ___; route evidence: ___ |
| Machine window and yield | ___; speed, dwell, pressure and failures: ___ |
| Full build including auxiliaries/fitments | ___; approved revision: ___ |
| Edge-of-window strength and integrity | ___; methods / results: ___ |
| Cost per good pack including trials/scrap | ___; consistent cost basis: ___ |
The short answers are practical: no verified collection route means no automatic local recycling claim; a passing cold peel test alone does not establish leak integrity; and unqualified shelf life blocks replacement. Use comparing film specifications to organize the supporting documents.
Sources and method
- CEFLEX design choices: mono-polyolefin preference and the effect of barrier layers, coatings, adhesives and inks. This is design guidance, not a local collection guarantee.
- ASTM F88/F88M-23: strip separation force, not package-leak detection; F1921/F1921M-12(2023): hot seal strength.
Public sources checked 9 October 2026. The tables are editorial comparison and assessment records with unfilled project values, not matched experimental data. No thickness, barrier, cost or machine-speed ranking is inferred.
Continue reading
Related articles
Mono-Material Packaging: Mono-PE and Mono-PP Flexible Structures
Mono material packaging explained: how mono-PE and mono-PP structures are built, their barrier limits, and what they change on the packaging line.
Mono-PE Packaging: Polyethylene-Based Pouches and Laminates
Mono PE packaging replaces PET/PE laminates with polyethylene-based films. See the outer webs, barrier options, seal window and machine changes involved.
Mono-PP Packaging: Polypropylene-Based Structures
Mono-PP packaging uses a PP-dominant structure. Check outer and sealant grades, cold-use and retort evidence, barrier, and recycling-stream compatibility.